Dies ist eine alte Version des Dokuments!
Scale-Up Module
The scale-up module serves for the transfer of processes to machines with larger and smaller diameters respectively. Starting from a so called model process, the geometry of the master design and the respective process parameters are calculated on the basis of transfer rules. The starting point of the scale-up is a user-defined complete process. A scale-up of processes with more than one feeding barrel is possible with SIGMA.
Selection of the Target Machine
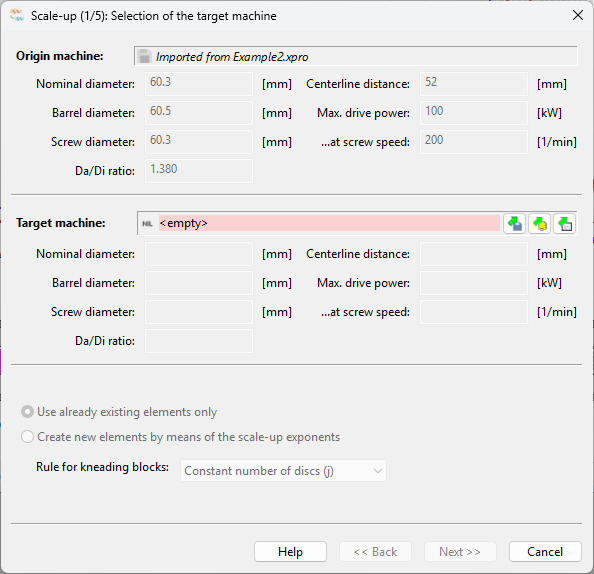
The Scale-up button opens the dialogue box shown in the illustration. The upper part of this box displays the machine data for the output process. An Explorer window allows you to select the machine to which the current process is to be transferred.
The procedure for selecting the elements is defined in the lower third of the dialogue box. The default setting is ‘Use existing elements only’. This ensures that only the screw and cylinder elements stored in the element library are used. With this procedure, the quality of the transfer depends heavily on the number of elements available in the library.
Alternatively, SIGMA 7 can generate fictitious elements that meet the requirements of similarity theory. This provides the optimal transfer result from a similarity theory perspective. By comparing the simulation results of both procedures, the influence of individual elements on the process can be better assessed.
In the latter case, the generation of screw and cylinder elements, it may also be necessary to select a transfer rule for the kneading blocks. This is always necessary when the model and main designs have different L/D ratios. There are three options to choose from:
- Equal number of kneading discs in main and model machine
- Constant staggering angle α
- Constant staggering angle and constant number of discs
Especially energy input, melting behavior, and degree of mixing are strongly influenced by the chosen law. The results have to be evaluated by the user for the unique process.
Setting of the Exponents
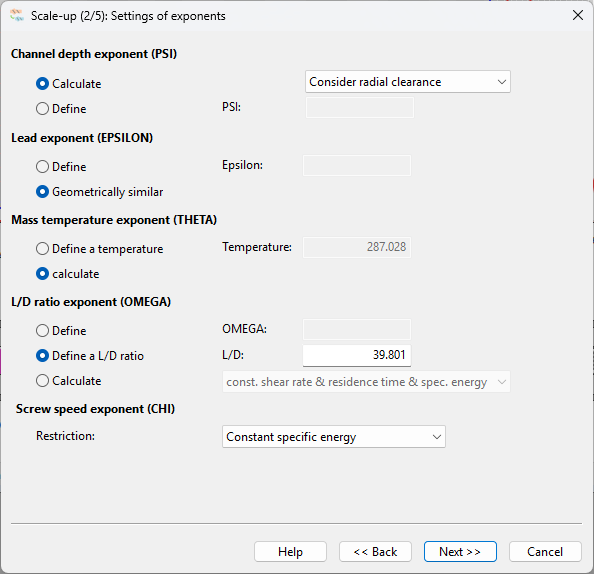
After pressing the Continue button, boundary conditions and specifications for the transfer can be defined. Of particular importance are the L/D ratio and the boundary conditions for the transfer of the operating point. Other options are more experimental in nature, such as defining the gear pitch exponent (EPSILON) or the mass temperature exponent (XI). Normally, the default settings should be retained here, as any change to these variables always violates the assumptions of similarity theory.
The pitch depth exponent (PSI) is calculated from the geometric data of the machines, as described in the basic manual. Here, it is possible to take the radial clearance into account or to ignore it. This directly influences the throughput and speed of the main design.
SIGMA is programmed so that the L/D ratio of the model design is adopted as a suggestion for the main design. Nevertheless, the user can freely select the length of the machine to be generated by specifying the L/D ratio or the corresponding OMEGA exponent. This makes it possible to trim the screw configuration to one of the actually available construction lengths.
It is also possible to consider the L/D ratio of the main design as a free variable. This is done by selecting the Calculate option in the L/D exponent (OMEGA) column. The length of the main design is then determined in such a way that the conditions listed in the Speed Exponent (CHI) column, constant shear velocity and constant residence time, are fulfilled simultaneously. In this case, it is no longer possible to select an additional boundary condition for the speed exponent.
If you specify an L/D ratio for the main design or accept the value suggested by SIGMA, you must select a boundary condition for the transfer of the operating point in the Speed Exponent (CHI) column. There are five options to choose from here:
- Constant specific energy input (s. Constant Specific Energy)
- Constant heat flow density (s. Constant Heat Flow)
- Constant shear rate
- Constant barrel temperature
- Constant residence time (s. Constant Residence Time)
The choice of boundary condition has a significant influence on speed and throughput. However, the values to be achieved are also a function of the PSI depth of cut exponent. For this reason, the selected transfer conditions must be assessed on a case-by-case basis. However, it can be said that in practice, process transfer is usually based on the conditions of constant specific energy input and constant average shear rate.
It should be noted that as the throughput increases, so do the requirements for heat transfer. This can lead to large temperature inhomogeneities in the melt, which may result in a significant increase in the mass temperature.
Further Information:
Calculation of the Exponents
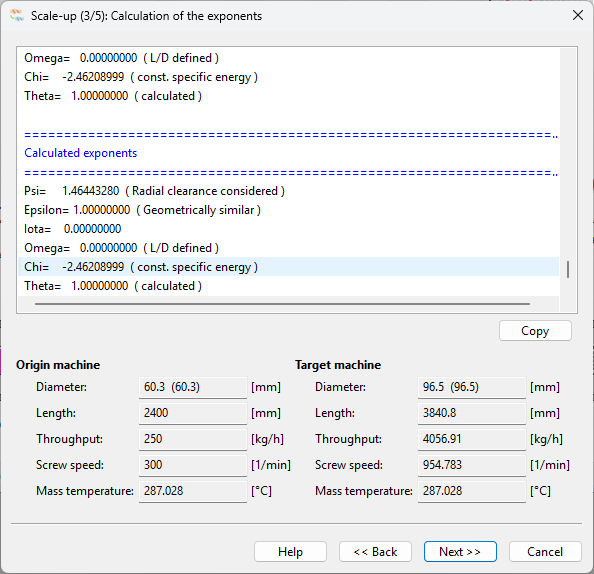
By activating the Next button an iterative calculation of the model law exponents is carried out. On the basis of these exponents, at first the process parameters are calculated and illustrated in the dialog (see figure).
Calculation of Screw and Barrel Configurations
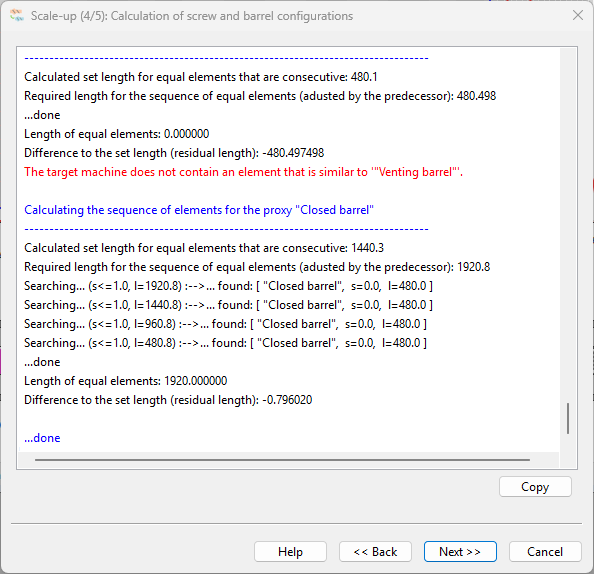
Subsequently, the screw and the barrel are generated. While applying the elements of the construction kit, the quality of the generated process generally increases with the amount of different elements.
All steps carried out during the configuration of the screw and the barrel can be reproduced by means of the dialog window (see figure).
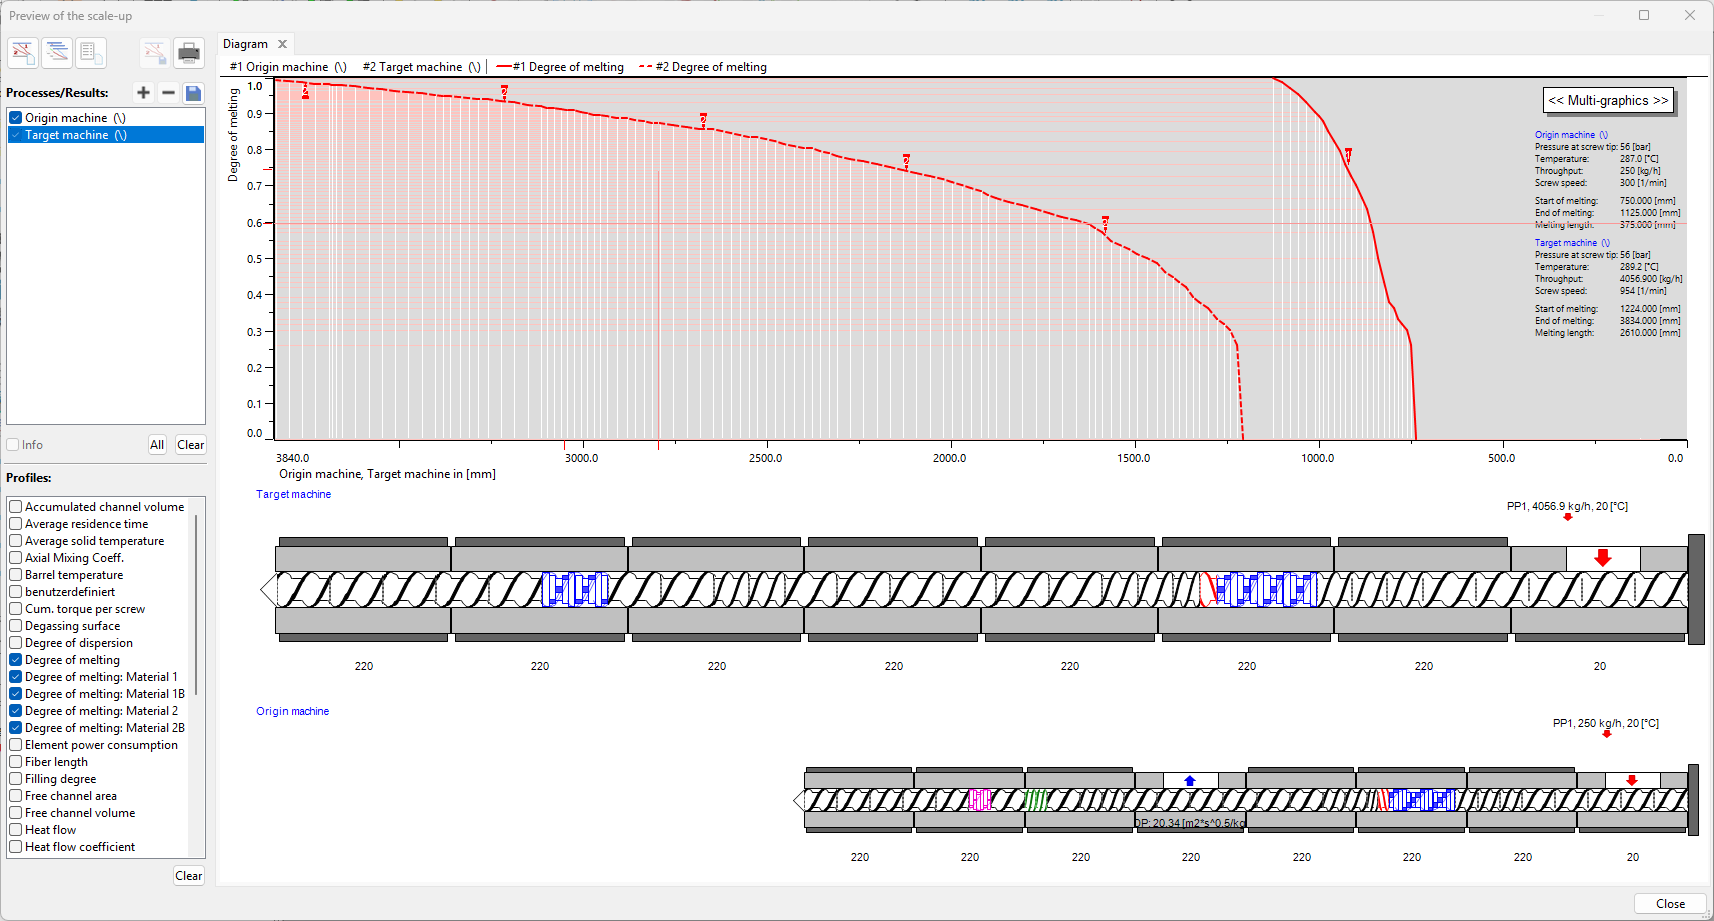
After confirming again, a preview of the simulation results is shown in a multi-graphic form (see figure). This enables a first comparison of both processes. Additionally, the operating parameters of the model design and the master design are displayed. While performing a scale-up it is possible to modify boundary conditions by means of the Back button.
Complete
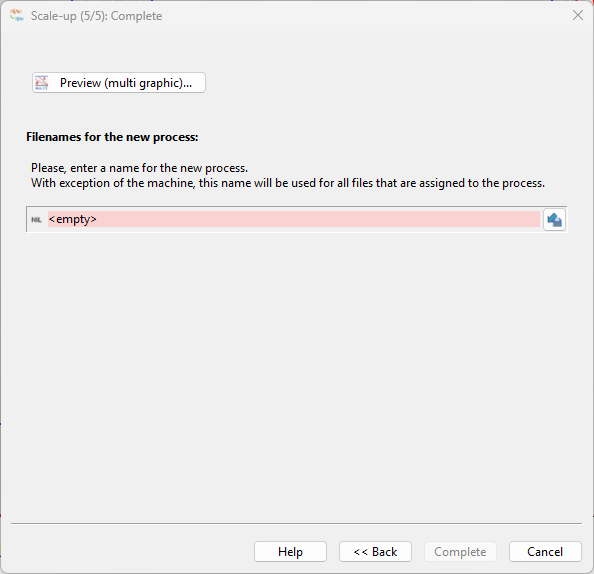
After closing the preview, the newly generated process can be saved by specifying a name and by pressing the Finish button afterwards.
The generated process is independent and can be loaded, changed and saved anew like any SIGMA process.